
Understand the operational problem.
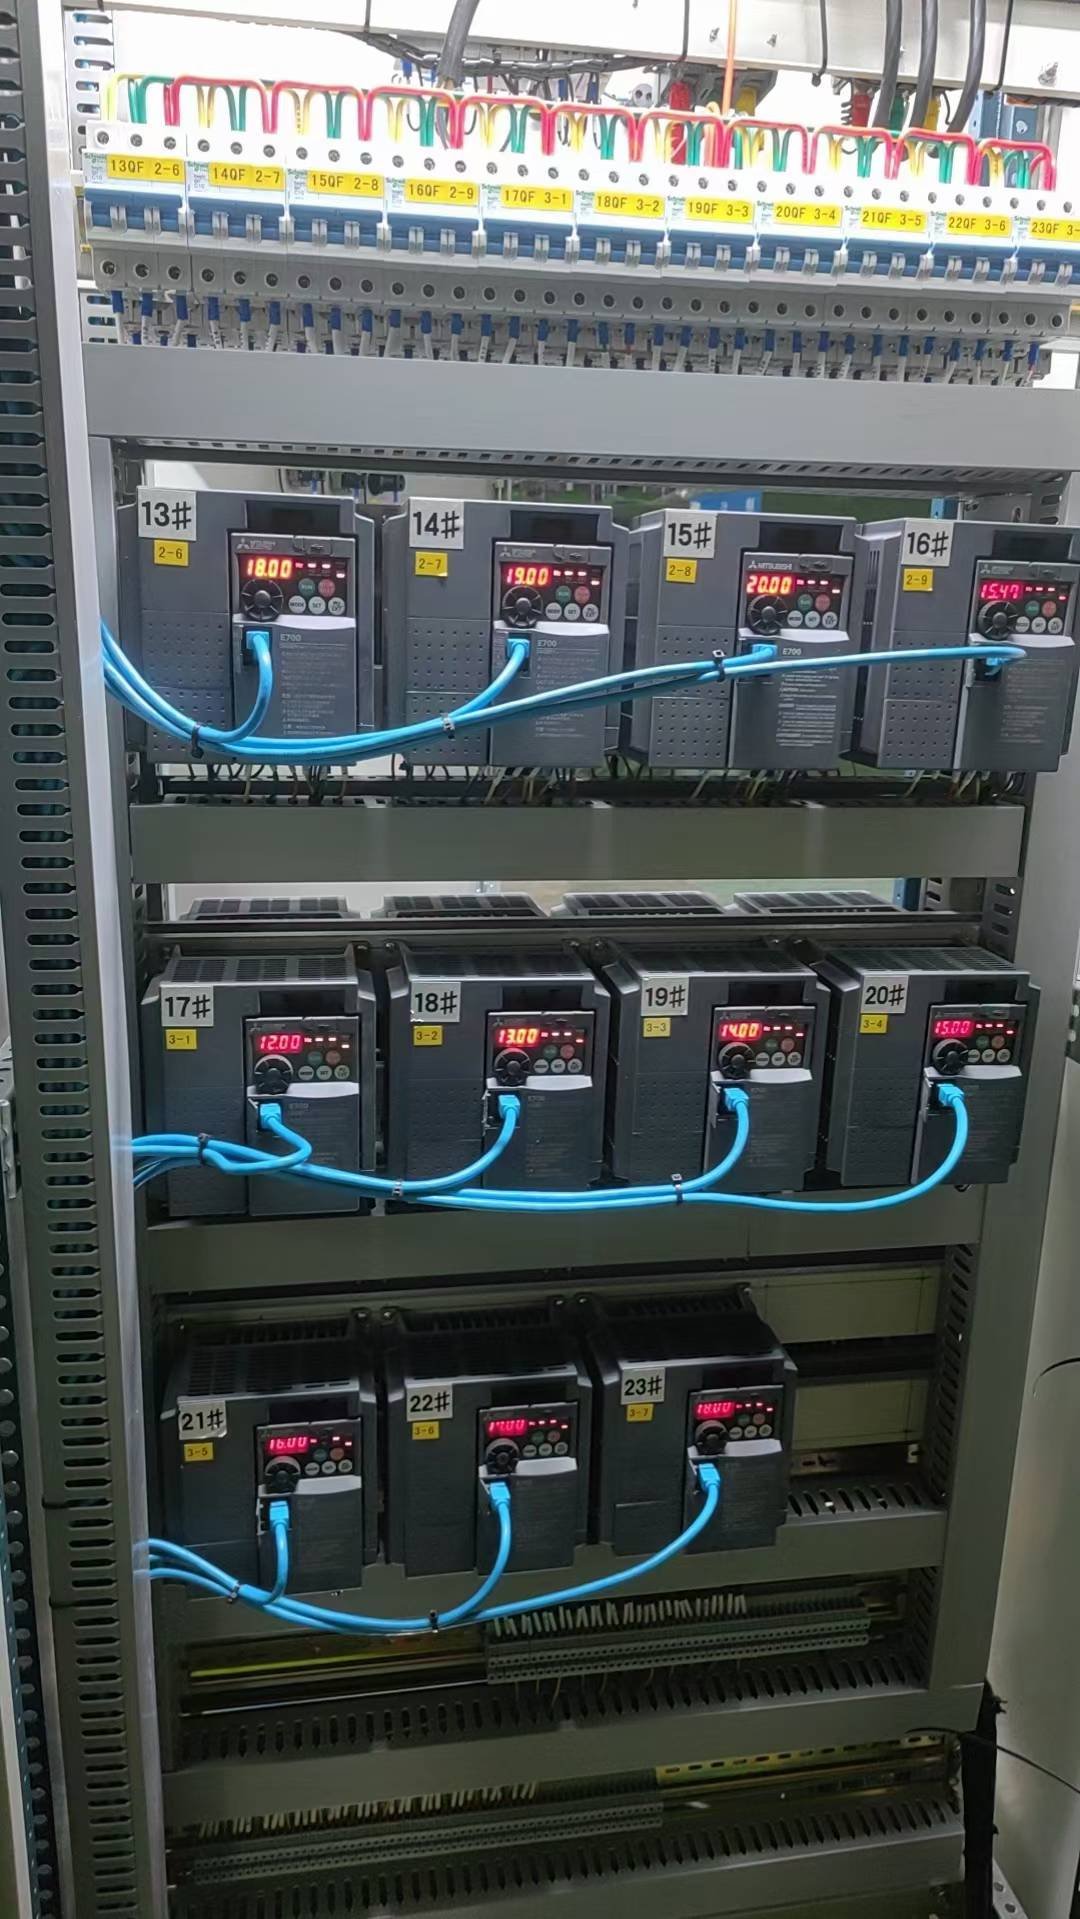
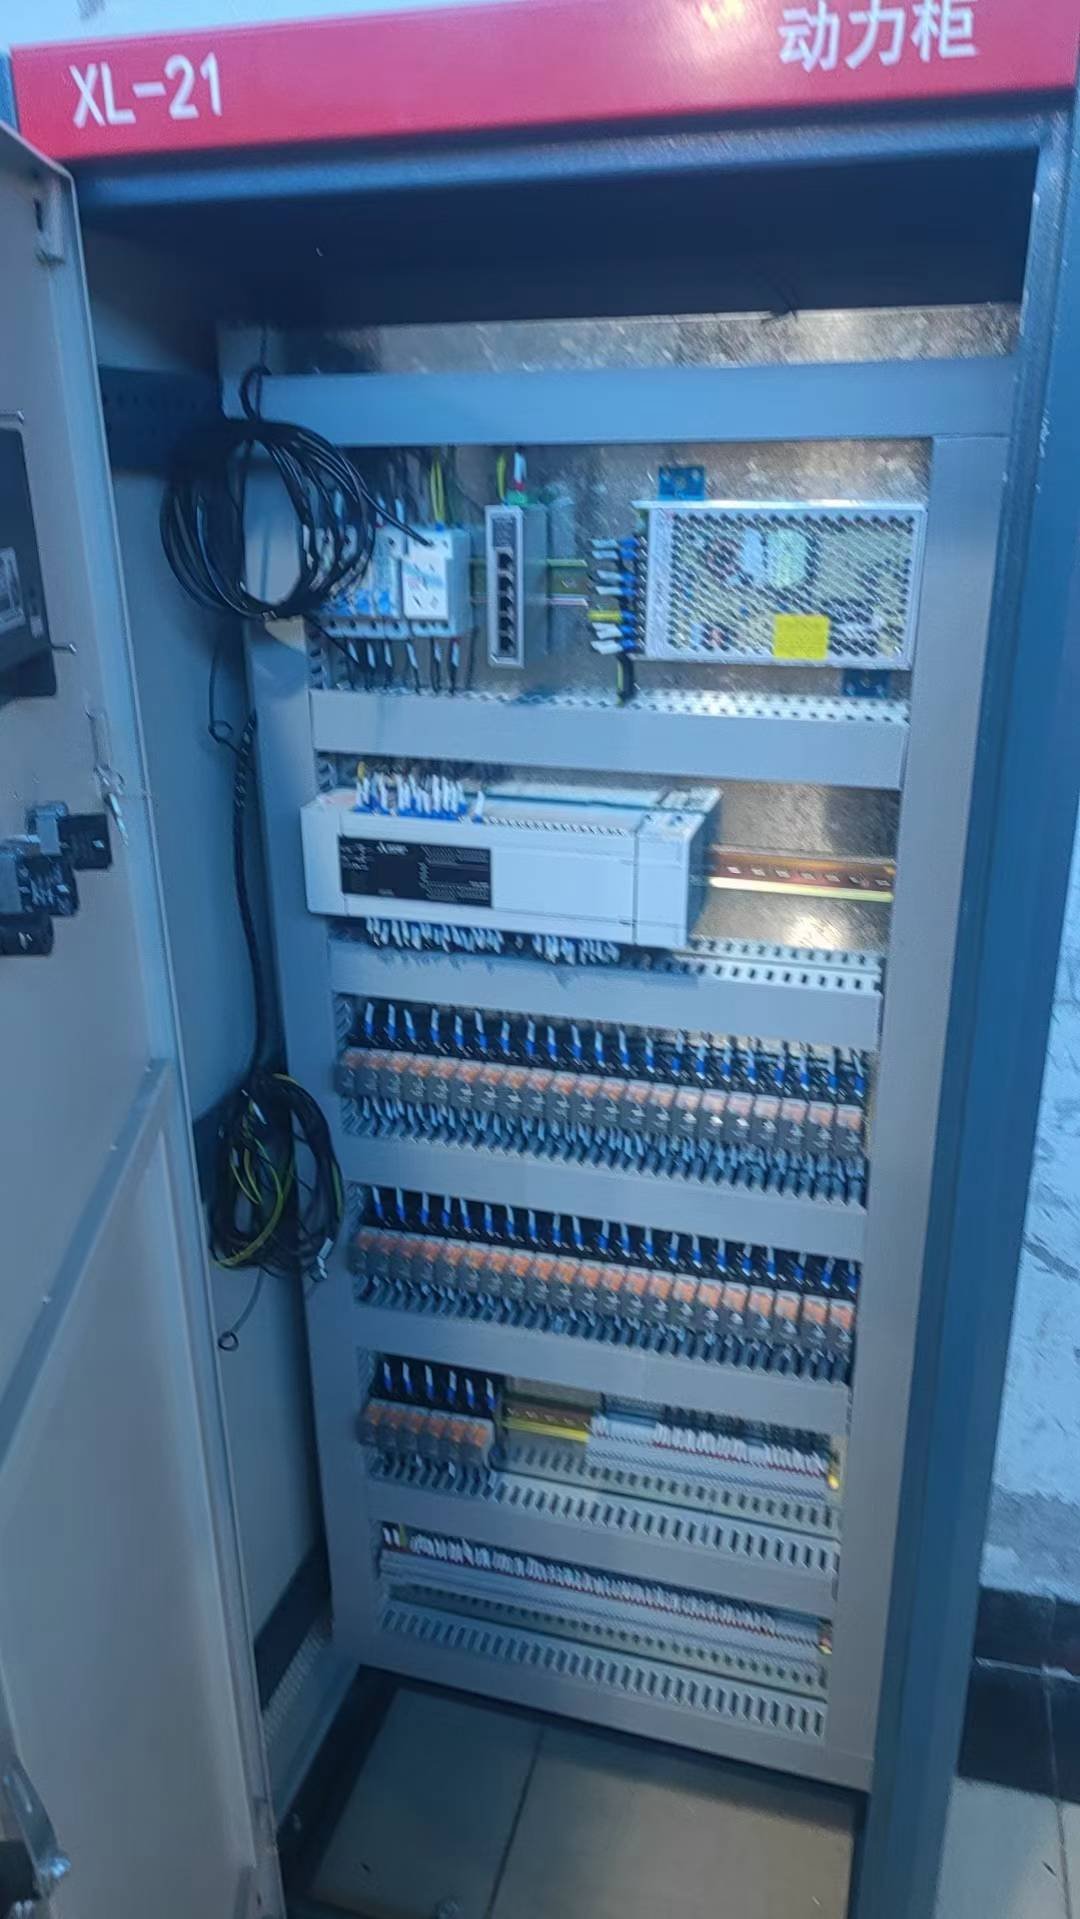
The published project uses a Mitsubishi FX5U PLC with drives and an HMI to control a multi-level conveyor. The English summary omits the customer name and location.
Project at a glance
- Application
- Multi-level conveyor with grouped drive operation
- Documented interface
- Automatic line operation and individual manual functions
- New-project discussion
- Existing-function preservation and agreed fault behaviour
The control challenge
The system needs convenient line-level operation while preserving individual motor functions for agreed commissioning and maintenance tasks.
Bring the layers together.
Conceptual control structure — an illustration, not a project screenshot or live data.
Separate the operating modes
Organise automatic line start/stop and frequency settings separately from individual manual motor functions.
Expose useful drive information
Group device status, running frequency, output voltage and output current by conveyor area.
Make exceptions traceable
Provide current and historical alarm views, role-based operation and I/O monitoring documented in the source case.
What this example demonstrates.
The original article reported the conveyor in operation at the time of publication. We do not treat that report as a fresh site inspection or claim unmeasured productivity gains.
The gallery contains the drive-cabinet and PLC-cabinet photographs from the company’s published article. They document the project at the time photographed; the separate control-chain visual is an explanatory illustration.
The live condition of the equipment has not been reverified for this website. Manual functions and emergency-stop interfaces require application-specific safety review.
Read the original Chinese caseA similar application starts with your equipment.
Use this case as a discussion reference. The actual hardware, control sequence, interfaces and acceptance conditions need to be agreed for your project.